Want to Discuss Your Upcoming Product Line?
Hinah coating will help you get things done.
Email us
Tel (Whatsapp/Wechat)
+86-186 3213 8668
Home » Products » Manual Powder Coating Line » Manual Powder Coating Line for Fire Doors
Manual Powder Coating Line for Fire Doors
Flexible and efficient coating system.
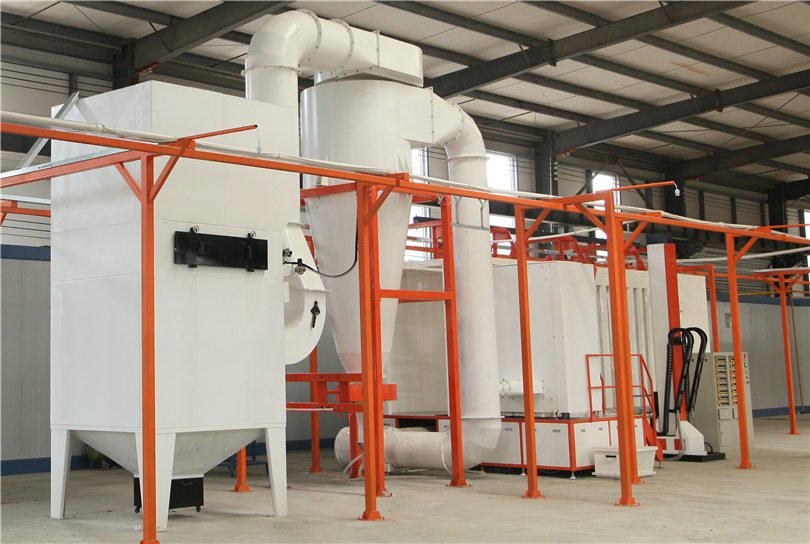
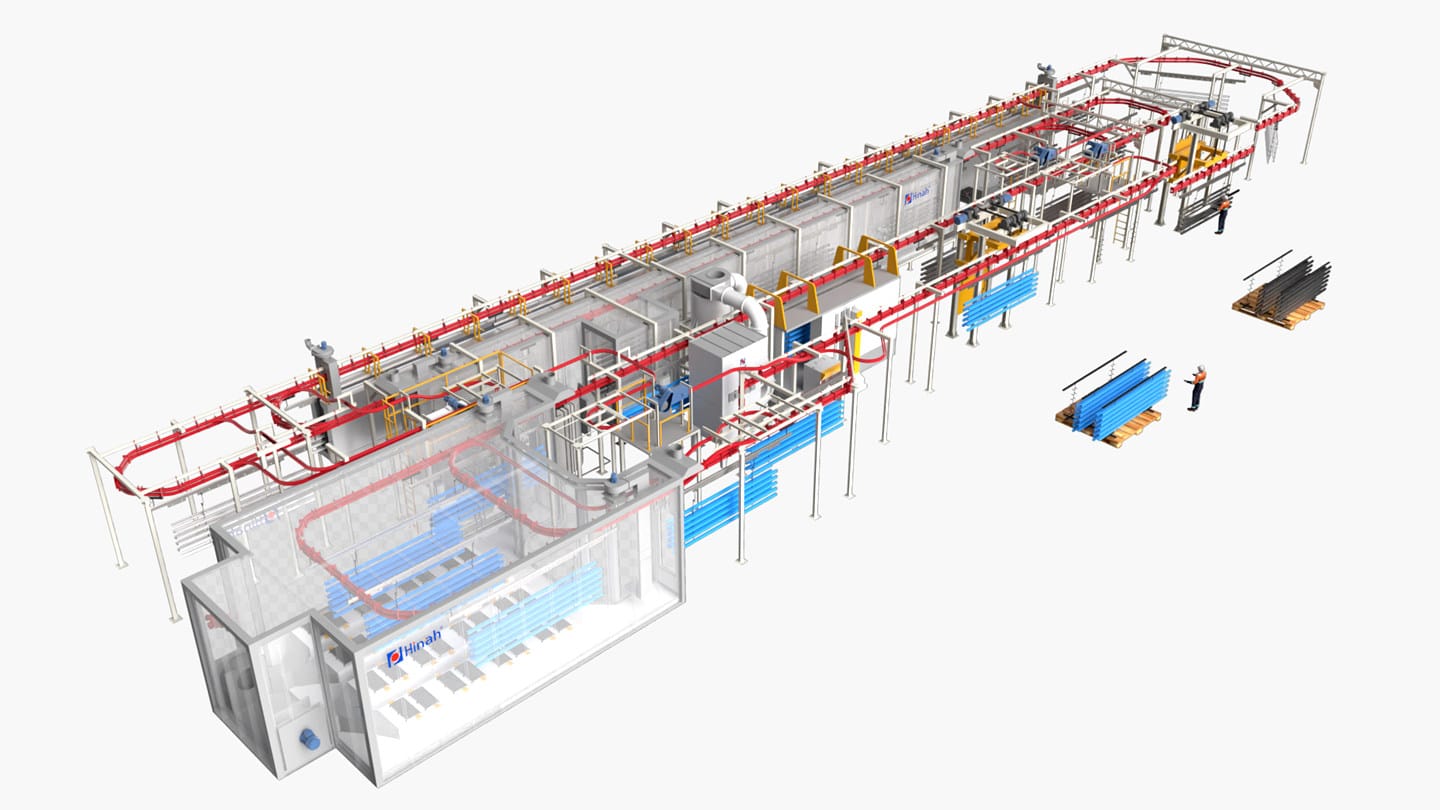
Process Flow: Loading– Pre-Treatment –Drying–Manual Powder Coating –Curing –Cooling –Unloading
1. Workpiece Name: Fire Doors
2. Maximum Size: L2400 × W500 × H1500 mm
3. Area Size: 19 m × 15 m
4. Heating Method: Natural Gas
5. Conveying Specifications: Semi-Auto Type
Fire doors are among the most unforgiving workpieces in powder coating. A leaf looks like a flat panel, but it is a folded steel skin wrapped around a mineral core, with a lock seam down both long edges, hinge and lock cut-outs that must stay bare, an intumescent strip groove that must stay clear, and two faces that are both in view once the door is hung. Every one of those features is either a place powder cannot reach, or a place where the film must not be. This page describes how the manual line is arranged around them: how the leaf is jigged and turned, where the operator changes angle, what is masked before the leaf enters the booth, and how film is measured so the door still closes on its seal.
The leaf is jigged through the hinge holes and travels upright. Hanging from the hinge holes does three things at once: both faces can be reached without laying the leaf down, the panel cannot sag under its own heat in the curing oven, and the folded edge sits at a workable height for the operator. The turn is a two-hook operation — an empty hook is brought alongside, the leaf is transferred at the hinge holes and rotated through 180 degrees, so the operator never touches a coated face. Lines without the second hook leave hand marks on the first face, and hand marks in a wet film do not flatten out in the oven.
The spray sequence follows the geometry, not the clock. Each leaf is coated along the lock seam first, then the hinge edge and the hardware cut-outs, then the two faces from the perimeter inward, and the perimeter of the second face last so that wrap-around lands on an area that has not been built up. At the fold the operator changes the gun angle rather than the distance, because a lock seam approached head-on stays empty no matter how much powder is put at it.
If the leaf is galvanized rather than cold-rolled, read the pre-treatment system page first — the chemistry and the dry-off change.

What a fire door demands from the coating process
Fire door leaves are normally built from cold-rolled or galvanized steel sheet between 0.8 mm and 1.2 mm, with a folded perimeter of 15–25 mm around a mineral core that is usually 40–50 mm thick. The skin is thin, the core is heavy, and the two behave differently in an oven.
The geometry is the hard part. A leaf has a continuous lock seam down both long edges, two hinge edges that sit on a tolerance surface, and a hardware pattern — lock, closer, hinge pockets — that must remain bare. Powder is applied electrostatically, so the seam and the cut-outs are exactly where the film builds least.
A second constraint is fit. The hinge knuckle, the lock bore and the closer mounting are tolerance surfaces; once film passes the range the hardware was designed for, the leaf sits proud in the frame and stops closing on its seal. The intumescent strip groove and the certification label are the same kind of constraint — they are not painted surfaces, and no amount of touch-up makes them right afterwards.
Coating targets for this workpiece are typically 60–80 μm on visible faces for indoor leaves in C2–C3 environments, and 80–120 μm where the door is installed externally or in a C4 environment. Acceptance is usually specified as adhesion class Gt0–Gt1 to ISO 2409 or 4B–5B to ASTM D3359, with a neutral salt-spray requirement of 240–480 hours for indoor grades.
The three defects that decide whether a leaf passes
1. Bare steel inside the folded lock seam. The perimeter fold closes on itself, so no gun angle reaches the inside of the seam. Capillary action during cure pulls the film back from the fold and what remains is a few microns on a sharp corner — which is the first place a leaf rusts and the first thing an inspector looks at. The countermeasures are fabrication and sequence: a small radius instead of a knife edge, then a light pass along the seam at reduced output before the main coat. Film is measured on the seam itself, not on the adjacent face, because the face will always read acceptable.
2. Pinholes on the galvanized skin. Zinc and core moisture both release gas in the cure window, and a film that is too thick traps that gas until it breaks through. The fix is a controlled ramp instead of a fast climb, film kept inside the specified range rather than above it, and enough time at temperature for the gas to escape before the film flows closed. Overbuilding to cover a pinhole makes it worse.
3. Too much film at the hinge edge. Powder accumulates on edges, and the hinge edge is an edge on a tolerance surface. Once the film there passes the range the hardware was designed for, the leaf sits proud in the frame and stops closing on its seal. Spraying the edge first and building the face afterwards keeps the accumulation where it can still be controlled, and the hinge edge is measured as its own reading rather than as part of the face average.
A fourth issue is easy to miss: powder inside the intumescent strip groove. The strip has to expand into the gap under heat, and a coated groove reduces its adhesion and can hold it back. The groove is masked before the leaf enters the booth and unmasked before curing, or plugged with a silicone plug rated for the oven. The certification label is treated the same way — it stays readable.
What we need to size the line
Every manual powder coating line here is built to the workpiece. What we need from you: factory dimensions (length × width × height), leaf drawings with skin thickness, core thickness and the hardware cut-out pattern, daily output measured in leaves per 8-hour shift, powder type and colour-change frequency, and the film thickness and salt-spray grade required by your customer.
Proven
30 years of experience providing proven equipment
Lifetime Service
Maintenance is more important than repair
Maximum Efficiency
Production line capacity fully matches demand without wasting any resources
Contact Us -- Free Design & Order Equipment Calculation
Order Equipment Calculation
In Order To Provide You With The Best Solution, Please Tell Us The Following Information
● Factory Dimensions (length, width, height)
● Work Piece Output (1 day = 8 hours, 1 month = 30 days)
● Material of the workpieces
● Dimensions of work piece
● Weight of the workpieces
● Color Change Demand (Frequency)
We closely communicate with clients to understand their needs and provide tailored solutions. Once the solution fits their requirements, we customize the production of the powder coating line to help them adapt to their specific production environment and coating needs.
/CONTACT US
Want to Discuss Your Upcoming Product Line?
Hinah coating will help you get things done.
Email us
Tel (Whatsapp/Wechat)
+86-186 3213 8668
Learn How We Helped 1000+ Customers Gain Success.